How to Choose Welding Equipment for Mass Production Lines

Time:2026-10-12 Author:Amelia
0%

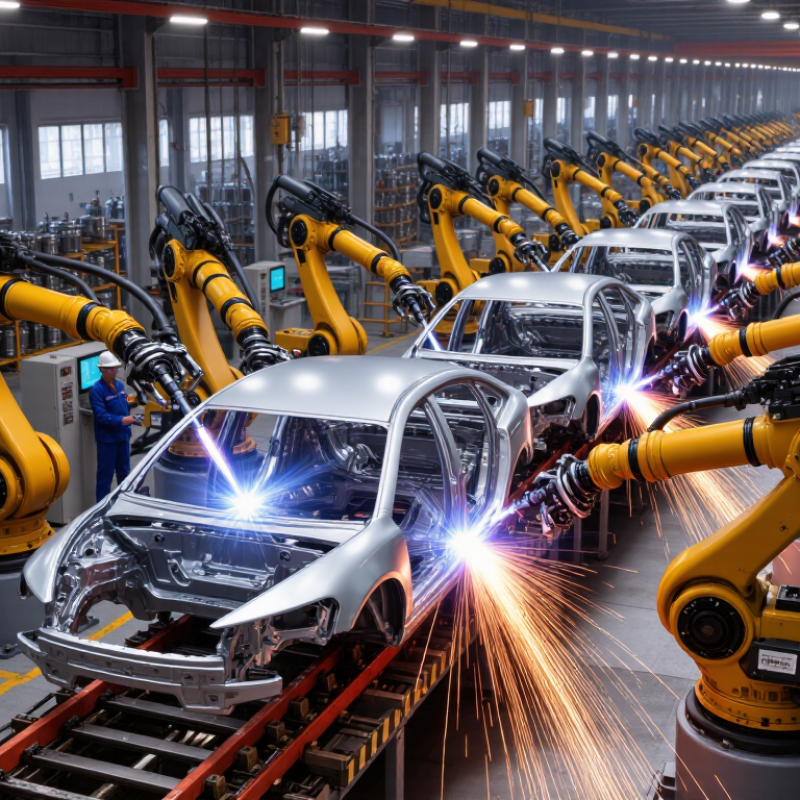
How to choose welding equipment for mass production lines is a production decision, not merely a machine purchase. It affects cycle time, weld consistency, operator safety, maintenance, and total cost per part. The International Federation of Robotics reported more than 541,000 industrial robots installed worldwide in 2023. Automotive manufacturing remained one of the largest adopters. This trend shows why robotic welding deserves serious evaluation, especially where thousands of identical joints repeat daily.

Start with the product and its production reality. Examine material grade, thickness, joint design, weld length, tolerance, and required output. MIG/MAG systems may suit high-volume steel fabrication, while laser welding can reduce heat distortion on suitable thin components. Resistance welding remains effective for sheet-metal assemblies. The American Welding Society and ISO 3834 emphasize qualified procedures, traceability, inspection, and consistent quality controls. A fast system without reliable monitoring can create expensive hidden defects.

Dr. John C. Lippold, a recognized welding metallurgy authority, wrote, “Weldability is not an inherent material property, but rather a characteristic of a material in a specific welding process.” His point is practical. Equipment must match the material, consumables, fixture, and production environment together. Grand View Research estimates continued growth in the global welding equipment market, driven partly by automation and manufacturing investment. Yet market growth does not guarantee a correct purchase. A perfect first choice is unlikely. Pilot trials, sample welds, downtime records, and operator feedback should guide the final decision. The cheapest machine may become the costliest one beside a stopped conveyor.
How to Choose Welding Equipment for Mass Production Lines

Define Production Requirements and Welding Specifications

Choosing welding equipment for a mass production line starts with clear production requirements. Define the daily output, takt time, material types, thicknesses, and joint designs. Record the required weld length and acceptable defect limits.

Do not select equipment from output numbers alone. A line producing 500 assemblies may need different capacity than a line producing 500 simple brackets. Calculate duty cycle, arc-on time, fixture loading time, and cooling requirements.

Check whether the power supply can support repeated welds without unstable performance. Small details matter.

Welding specifications should describe current range, voltage, wire or electrode size, shielding gas, travel speed, and preheat needs. Include weld position and access limitations. These details help engineers match the process with the equipment, fixture, and automation level. Sample welds should be tested before approval. Visual inspection is useful, but it cannot reveal every internal problem. Consider dimensional checks, bend tests, or other suitable inspections based on the joint and application.

Traceability also deserves attention. Record weld parameters, operator settings, material batches, and inspection results. This supports consistent production and faster troubleshooting. In practice, specifications are sometimes copied from older projects without enough review. That is risky. A previous setting may work poorly with a new thickness or joint gap. Leave room for controlled trials and documented adjustments. Perfect assumptions rarely survive the factory floor.

Compare Welding Processes for Speed, Quality, and Material Compatibility

Choosing welding equipment for mass production starts with the joint, not the machine. Process speed, weld quality, and material compatibility must be measured together. The AWS Welding Handbook reports typical GMAW deposition rates of about 3–8 kg per hour, while GTAW often stays below 1 kg per hour. GMAW suits carbon steel and aluminum assemblies, but shielding gas and spatter require control. GTAW produces cleaner, precise welds on thin stainless steel, yet its slower travel can restrict output. Resistance spot welding is extremely fast for overlapping sheet metal, with many cycles completed in less than one second. It is less suitable for thick sections or complex joint access.

Laser welding can deliver narrow heat-affected zones and high travel speeds. However, it demands accurate fit-up and stable surface conditions. A small gap can cause porosity or incomplete fusion. The International Federation of Robotics’ World Robotics 2024 report recorded 541,302 industrial robot installations globally in 2023. That figure reflects strong automation demand, but automation cannot repair poor joint design. ISO 5817 quality levels can help define acceptable weld imperfections before equipment selection. That step is often skipped.

Tips: Test representative parts, not polished samples. Record cycle time, gas use, rework, distortion, and operator adjustments. For a high-volume line, compare total cost per acceptable weld. A faster process may create more inspection work. Trial results may challenge the original plan. That is useful. Pair visual checks with destructive testing and cross-section reviews. Reserve enough space for fume extraction, torch maintenance, and safe material handling.

Choosing Welding Equipment for Mass Production Lines

Comparison of common welding processes using typical industrial ratings for production speed, weld quality, and material compatibility. Ratings are based on general process characteristics and may vary with joint design, material thickness, automation, and operating parameters.

Evaluate Equipment Capacity, Automation, and Integration Options

How to Choose Welding Equipment for Mass Production Lines

Evaluate capacity against the real production rhythm, not the supplier’s maximum rating. A machine rated for 60 welds per hour may deliver fewer under continuous heat, repositioning, and inspection delays. Measure takt time, duty cycle, wire consumption, and planned maintenance hours. The International Federation of Robotics reported 541,302 industrial robots installed worldwide in 2023. This shows automation is mainstream, but robot ownership alone does not guarantee output.

Check automation at the process level. Automatic seam tracking, torch cleaning, fixture sensing, and recipe control can reduce operator variation. The American Welding Society’s 2023 workforce study estimated that the industry may need 330,000 new welding professionals by 2028. That shortage makes repeatable automation valuable. Still, poor programming can multiply defects quickly. Human oversight remains necessary.

Integration deserves equal attention. Confirm whether equipment supports open communication protocols, production-monitoring systems, safety circuits, and quality records. Test data exchange before purchasing. A useful pilot should run representative parts, including awkward joints and short batch changes. Record arc-on time, rework, changeover minutes, and downtime. Do not trust a perfect demonstration. Real factories are less tidy. Review expansion capacity, spare-part access, training, and cybersecurity controls. The wrong interface can turn an efficient cell into an isolated island.

How to Choose Welding Equipment for Mass Production Lines - Evaluate Equipment Capacity, Automation, and Integration Options

Equipment Category Typical Welding Process Recommended Output Range Typical Duty Cycle Automation Level Production Capacity Indicator Integration Options Best-Fit Production Scenario Key Evaluation Point
Manual Constant-Voltage Power Source Gas metal arc welding using solid or flux-cored wire 250–400 A at approximately 25–35 V 40%–60% at rated output Low Suitable for low-volume work, repairs, prototypes, and variable product mixes Basic remote control, weld data logging, and optional wire feeder Job-shop production and stations requiring frequent operator adjustment Check arc stability, wire-feed consistency, operator ergonomics, and consumable cost
Industrial Pulse Welding System Pulse gas metal arc welding for steel, stainless steel, or aluminum 300–500 A at approximately 28–40 V 60%–100% at rated output Medium Supports repeatable welds at medium-to-high production volumes Digital I/O, fieldbus communication, recipe storage, weld monitoring, and robot interfaces Automotive components, fabricated assemblies, and products with repeatable joints Evaluate waveform control, parameter repeatability, data access, and heat-input control
Robotic Arc-Welding Cell Gas metal arc welding, pulse welding, or tandem arc welding 300–600 A per welding circuit 60%–100% at rated output High Often supports approximately 20–60 weld assemblies per hour, depending on joint length and handling time Robot controller, PLC, safety circuits, positioners, vision systems, MES, and production databases High-volume products with stable part geometry and repeatable weld sequences Assess takt time, reach envelope, fixture changeover, collision avoidance, and recovery procedures
Multi-Station Robotic Line Coordinated arc welding with automated part handling 300–600 A per welding station 70%–100% at rated output High Designed for continuous flow; line capacity is normally determined by the bottleneck station PLC line control, conveyors, automatic fixtures, barcode or RFID tracking, SCADA, and MES connectivity Large-volume production with several weld operations and defined takt time Verify line balancing, buffer capacity, maintenance access, and fault-isolation strategy
Resistance Spot-Welding System Resistance spot welding for overlapping sheet metal 6–25 kA secondary welding current, application-dependent Intermittent duty; cycle rating depends on transformer and cooling system High Can produce several spots per minute when part presentation and electrode access are optimized PLC, robot controller, weld-current monitoring, electrode force feedback, and traceability software Sheet-metal assemblies requiring many repeatable spot welds Check electrode life, water cooling, weld-current control, force accuracy, and access to each spot
Laser Welding Cell Fiber-laser welding with automated beam delivery 1–6 kW laser power for common industrial sheet and component applications Typically continuous operation with controlled thermal management High High travel speeds are possible, but actual throughput depends on fit-up, joint design, and inspection requirements Robot or gantry, seam tracking, vision inspection, safety enclosure, PLC, and process monitoring Thin-to-medium gauge parts, precise seams, and applications requiring low distortion Evaluate joint fit-up tolerance, laser safety, shielding-gas control, optics protection, and inspection method
Submerged Arc Welding System Submerged arc welding with one or more wire electrodes 600–1,500 A, depending on wire configuration and joint design 80%–100% at rated output Medium High deposition rates for long, straight welds; not suited to short or highly variable joints Travel carriage, seam tracking, flux recovery, PLC control, and weld parameter logging Heavy structures, pressure-related fabrication, beams, vessels, and long circumferential seams Confirm weld length, part rotation method, flux handling, heat input, and post-weld cleaning needs
Automated TIG Welding System Gas tungsten arc welding for precision joints 200–400 A, depending on material and thickness 40%–100% at rated output Medium Lower deposition rate than arc-wire processes, but strong consistency for clean, high-quality welds Motorized torch slide, orbital head, AVC, oscillation control, PLC, and weld data recording Stainless tubing, precision components, aerospace-style fabrication, and hygienic assemblies Prioritize shielding quality, joint cleanliness, arc-length control, and fixture repeatability
Automated Welding Positioner Supports MIG/MAG, TIG, or submerged arc welding Load capacity commonly 100–10,000 kg, application-dependent Based on motor, gearbox, and thermal design Medium Can reduce repositioning time and improve weld access, especially for circumferential or multi-axis work PLC, robot synchronization, servo control, encoder feedback, and safety interlocking Parts requiring multiple welding orientations or controlled travel speed Check payload at offset center of gravity, rotational accuracy, indexing time, and cable management

Note: Capacity figures are practical planning ranges rather than guaranteed production rates. Final selection should be validated through time studies, weld procedure qualification, fixture trials, utility checks, and integration testing using the actual part geometry and material.

Assess Safety Features, Maintenance Needs, and Operating Costs

Choosing welding equipment for a mass production line requires more than comparing arc speed. Safety features, maintenance demands, and operating costs often determine whether a line remains profitable. The International Federation of Robotics reported 541,302 industrial robots were installed worldwide in 2023. This growth increases the need for guarded cells, interlocked access doors, emergency stops, torch collision protection, and verified light curtains. Equipment should also support fume extraction and stable grounding. A faster machine is not safer by default.

Maintenance details deserve close inspection. Ask how quickly operators can replace liners, contact tips, filters, and cooling components. A clear fault display can save hours beside a silent, overheated power source. The U.S. Department of Energy notes that maintenance may represent 15% to 40% of manufacturing costs, depending on the facility and process. That range is broad, but it exposes a common mistake: purchasing price is often treated as total cost. Record service intervals, spare-part availability, training time, and unplanned downtime before approval.

Operating cost calculations should include electricity, shielding gas, wire waste, consumables, labor, and rejected welds. The Deloitte 2024 Smart Manufacturing and Operations Survey found that manufacturers increasingly prioritize productivity, quality, and resilience together. These goals can conflict. Higher travel speed may increase spatter or inspection work. In practical trials, measure energy per acceptable weld, not energy per operating hour. My own caution is simple: spreadsheet estimates rarely survive a dusty production floor. Pilot testing under real shift conditions may reveal maintenance work that specifications omit.

Validate Equipment Through Testing, Training, and Performance Monitoring

Choosing welding equipment for mass production should begin with evidence, not catalogue specifications. Test the system using actual materials, joint designs, wire sizes, and production speeds. Record bead width, penetration, spatter, arc-on time, and rejection rates. Inspect test coupons through visual checks and suitable non-destructive methods.

Run the trial across several shifts. Different operators expose different weaknesses. A stable process should survive starts, stops, fixture changes, and minor material variation. It may not. That failure is useful. Investigate it before installation becomes expensive.

The International Federation of Robotics reported 541,302 industrial robots were installed worldwide in 2023.

Automation is growing, but validation still determines whether equipment performs reliably.

Training must match the equipment and the work cell. Teach operators parameter control, fixture checks, defect recognition, and safe recovery procedures.

The World Economic Forum’s Future of Jobs Report 2023 estimated that 44% of workers’ skills could change by 2027.

Short demonstrations are not enough. Use practical assessments and refreshers after process changes. Monitor first-pass yield, downtime, consumable use, alarms, and weld-quality trends weekly. Keep records by operator, shift, material, and machine.

Data can reveal gradual drift before defects become visible. Yet dashboards can mislead when sensors are poorly calibrated or data is incomplete. Review unusual results manually. Adjust thresholds carefully.

A production line needs disciplined measurement, but experienced judgment still matters.

FAQS

What production details should be defined before selecting welding equipment?

Record daily output, takt time, materials, thicknesses, joint designs, and required weld lengths. Small details matter. Include acceptable defect limits and cooling needs. A line making 500 simple brackets differs from one making 500 complex assemblies.

Why is output volume alone unreliable for equipment selection?

Output numbers hide fixture loading, arc-on time, cooling, and access conditions. Two lines may produce identical quantities. Their equipment capacity can still differ greatly. Check repeated weld stability and power supply performance.

Which welding process is suitable for fast, high-volume production?

Gas-shielded arc welding can provide roughly 3–8 kilograms of deposited metal hourly. It suits many carbon steel and aluminum assemblies. Shielding gas and spatter require control. Resistance spot welding is faster for overlapping sheet metal, often completing cycles under one second.

When might precision welding be a better choice than faster welding?

Precision arc welding suits thin stainless steel and applications needing clean, accurate joints. Its deposition rate often remains below one kilogram hourly. That may restrict output. Still, lower cleanup and better appearance can justify the slower cycle.

What limitations should be considered with laser welding?

Laser welding can create narrow heat-affected zones and high travel speeds. Fit-up must be accurate. A small gap may cause porosity or incomplete fusion. Stable surfaces and careful joint preparation are essential.

What information should a welding specification include?

Specify current, voltage, wire or electrode size, shielding gas, travel speed, and preheat requirements. Add welding position and access limits. The specification should match the fixture, joint, material, and automation level.

How should sample welds be tested before production approval?

Test representative production parts, not polished demonstration samples. Use visual inspection with dimensional checks, bend tests, cross-sections, or suitable destructive tests. Visual checks miss internal problems. The original plan may fail here.

How can a production line improve welding traceability?

Record weld parameters, operator settings, material batches, inspection results, gas use, and rework. These records support faster troubleshooting. They also expose repeated adjustments. Keep controlled trials documented, because copied settings may not suit new thicknesses or joint gaps.

What hidden costs should be compared between welding processes?

Compare the total cost per acceptable weld, not only machine speed. Include cycle time, gas consumption, distortion, inspection effort, rework, and maintenance. A faster process may create more rejects. That is easy to underestimate. Reserve space for fume extraction and safe material handling.

Conclusion

How to choose welding equipment for mass production lines begins with clearly defining production requirements, including material types, joint designs, product dimensions, welding positions, output targets, and quality standards. These details help manufacturers compare suitable welding processes according to speed, weld consistency, heat control, and material compatibility. The selected process should support reliable results while reducing defects, rework, and production delays.

Equipment capacity, automation level, and integration options are also essential considerations. Systems should fit smoothly into existing production lines and provide stable performance at the required workload. Buyers should further assess safety functions, maintenance access, spare-part needs, energy consumption, and total operating costs. Before final approval, the equipment should be validated through sample production, operator training, and performance monitoring. Reviewing weld quality, cycle time, downtime, and long-term stability will help confirm that the solution meets production goals and remains efficient as demand increases.
Amelia

Amelia

Amelia is a seasoned marketing professional with a wealth of expertise in our company’s core offerings. With an unwavering passion for driving growth and innovation, she plays a pivotal role in shaping our marketing strategies and enhancing brand visibility. A key aspect of her responsibilities......